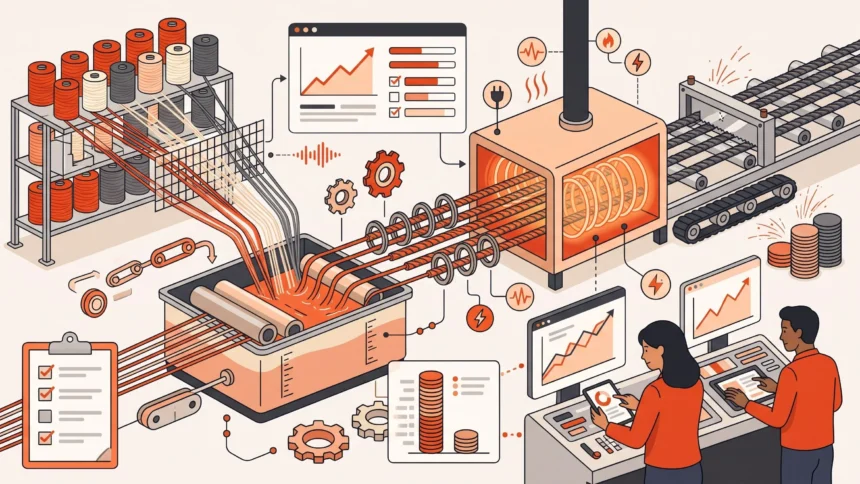
An industrial intelligence and unit-economics comparison of the Composite-Tech CT6 New Generation, Mashspetsstroy LISA-1, RZPO LPSPA-1, and Prowelltec Four Out – examining how illustrative multi-strand architecture assumptions, AI-assisted optical telemetry, and energy-per-meter metrics drive composite factory profitability.
- 1. Process Telemetry: How GFRP Rebar Pultrusion Machines Actually Work
- 2. Benchmarking GFRP Rebar Pultrusion Machines in 2026
- 3. Composite-Tech CT6 New Generation: Six-Bar Industrial Throughput
- 4. Process Engineering & Sensor Intelligence Inside the CT6
- 4.1 Multi-Stage & Ultrasonic-Assisted Resin Impregnation with Pneumatic Squeezing
- 4.2 Short-Wave Infrared (IR) Polymerization Booster
- 4.3 Two-Stage Thermal Gradient Management (Air + Water Cooling)
- 5. Mashspetsstroy LISA-1: Single-Strand Baseline Analysis
- 6. Evaluating Compact & Four-Strand Alternatives: RZPO and Prowelltec
- 6.1 RZPO LPSPA-1: Compact Single-Strand Concept
- 6.2 Prowelltec Four Out: Mid-Tier Four-Strand Manufacturing
- 7. The Unit Economics of Smart Pultrusion: Labor & Energy Telemetry
- 8. Multi-Fiber Platform Agility: GFRP, BFRP, CFRP, and AFRP
- 9. Quality Assurance, AI Optical Telemetry, and ASTM D7957 Compliance
- 10. Building a Complete Smart Composite Reinforcement Ecosystem
- 11. Due Diligence Checklist for Pultrusion Equipment Buyers
- Why Process Intelligence Drives Composite Factory ROI
- FAQ
- How do GFRP rebar pultrusion machines work?
- Which GFRP rebar pultrusion machine is best in 2026?
- What is the ROI of a GFRP rebar production line?
- Technical Sources, Standards, and Verification Links
Selecting GFRP rebar pultrusion machines requires auditing combined multi-strand linear output, resin wet-out efficiency, thermal curing zones, and steady-state kilowatt-hours per 1,000 saleable meters. Multi-strand platforms like the six-bar Composite-Tech CT6 New Generation lower unit conversion costs for infrastructure volume, while single-strand lines fit smaller regional shops.
Not long ago, a manufacturer entering the fiberglass reinforcement sector could build a solid business case around a single-strand production line making one reinforcing bar at a time. Under those baseline assumptions, for a local plant supplying modest volumes, the math worked out fine. Capital expenditure stayed low, mechanical supervision was straightforward, and manual quality checks sufficed.
That equation breaks down the moment a plant scales into enterprise infrastructure and regional distribution. According to MarketsandMarkets research on GFRP rebar companies, the global GFRP rebar market is projected to grow from USD 0.54 billion in 2025 to USD 0.95 billion by 2030 at a 12.1% CAGR. When a distributor orders tens of thousands of linear meters, a contractor demands multiple diameters on a tight schedule, or a public-sector project requires documented mechanical compliance under manufacturer-referenced ASTM D7957/D7957M-26 criteria, the pultrusion line stops acting like a standalone mechanical asset. It directly sets factory throughput, labor productivity, energy efficiency, and unit cost per saleable meter.
With Industry 4.0 and manufacturing analytics standards now common, evaluating modern glass fiber reinforced polymer (GFRP) rebar pultrusion machines requires looking past advertised peak pulling speeds. Decision-makers must audit combined multi-strand output, resin impregnation efficiency, thermodynamic curing profiles, two-stage cooling control, and real-time optical telemetry.
Among the industrial systems benchmarked in this comparison, Composite-Tech’s CT6 New Generation shows how process engineering and automated data supervision work together under published vendor specifications. Built to produce up to six reinforcing bars at once, the platform pairs high total throughput with closed-loop process controls across the composite production sequence. Below, we benchmark the CT6 against single-strand and four-strand alternatives using illustrative manufacturer-declared figures and outline the exact operational metrics capital investors should audit before commissioning a GFRP facility.
Important Engineering Caveat: No single machine fits every capital budget or niche facility based on linear speed alone. Optimal equipment selection depends on target diameter mix, structural code compliance, facility footprint, raw material compatibility, verified operating costs, and vendor commissioning support. All performance figures analyzed in this report reflect illustrative manufacturer-declared specifications instead of independent third-party comparative factory trials.
1. Process Telemetry: How GFRP Rebar Pultrusion Machines Actually Work
Fiberglass reinforcement manufacturing uses continuous composite pultrusion. Continuous glass fiber rovings pull from creels, pass through polymer resin impregnation modules, take shape as cylindrical bars, get helically wrapped or ribbed to create a mechanical bond profile for concrete interaction, and move through thermally regulated polymerization and cooling zones.
Standard Continuous GFRP Production Sequence: Fiber Feeding → Fiber Preheating & Preparation → Resin Impregnation → Bar Forming → Helical Rib Winding / Coating → Multi-Stage Polymerization → Controlled Cooling → Synchronized Pulling → Automated Cutting or Coiling.
More Read
Hardware execution varies across equipment tiers. Entry-level lines typically use open dip-tank resin baths and basic convective heating ovens. Advanced industrial platforms integrate multi-stage or ultrasonic-assisted wet-out systems, infrared thermal boosters, and automated tension controls designed to keep composite homogeneity stable at higher line speeds.
Why Single-Strand Pulling Speed Is a Vanity Metric
In manufacturing analytics, judging a pultrusion machine by its linear pulling speed per strand is a classic single-variable trap. Compare two lines running at the same linear velocity of 6 m/min:
Machine A (Single-Strand illustrative assumption): 1 bar × 6 m/min = 6 meters per minute combined output.
Machine B (Six-Strand illustrative assumption): 6 bars × 6 m/min = 36 meters per minute combined output.
Over an uninterrupted eight-hour shift, the theoretical output gap under these illustrative assumptions grows fast:
For the same illustrative 6 m/min strand speed, one bar yields 2,880 m, four bars yield 11,520 m, and six bars yield 17,280 m over an uninterrupted eight-hour shift. These are arithmetic scenarios, not measured factory outputs.
Scaling strand count takes more than bolting on extra pulling clamps. Multi-strand architecture brings tough multiphysics problems: the impregnation unit must wet out up to six fiber bundles evenly without micro-voids; the curing oven must hold uniform exothermic profiles across all channels; traction mechanisms must stop differential slippage; and downstream cutters must stay in tight sync.
2. Benchmarking GFRP Rebar Pultrusion Machines in 2026
To keep capital expenditure analysis grounded in published vendor figures, we compare four commercial models covering single-strand, four-strand, and six-strand industrial setups. Buyers must weigh multi-strand output against plant floor space, power capacity, and whether the vendor documents linear speeds by exact bar diameter.
Table 1. Industrial GFRP Rebar Production Equipment Comparison (2026)
The figures below were checked against working manufacturer pages: Composite-Tech CT6 capacity schedule, Mashspetsstroy LISA-1 specifications, RZPO LPSPA-1 catalogue on ASP37, and Prowelltec Four Out specifications. These pages support the stated configurations and nominal capacities; they do not establish independently measured comparative performance. Original submitted links are retained in the source list, including unavailable legacy pages. Confirm current specifications and sustained output during factory acceptance testing.
| Manufacturer | Model | Simultaneous Bars | Diameter Range | Published Production Capacity |
|---|---|---|---|---|
| Composite-Tech | CT6 New Generation | Up to 6 | 4-20 mm | 36 m/min combined at 10 mm; 48 m/min at 4 mm |
| Mashspetsstroy | LISA-1 | 1 | 4-16 mm | 3 m/min at 10 mm (8 m/min at 4 mm) |
| RZPO | LPSPA-1 | 1 | 4-14 mm | Diameter-specific combined output not clearly documented |
| Prowelltec | Four Out | 4 | 4-14 mm | 12,000-16,000 m per 24 hours; reference diameter unspecified |
Sources: The four manufacturer pages linked above. CT6 and LISA-1 rates are diameter-specific nominal figures. Prowelltec does not identify the reference diameter for its daily output, and RZPO does not provide a diameter-indexed speed schedule on the linked page.
Table 1 exposes a data transparency gap in industrial equipment procurement. Composite-Tech and Mashspetsstroy publish granular, diameter-specific linear speeds, whereas RZPO leaves out a diameter-indexed output table on its public LPSPA-1 page, and Prowelltec quotes an illustrative 24-hour volume (12,000-16,000 m) without linking that number to a specific bar diameter. Note that Mashspetsstroy (LISA-2, LISA-4) and RZPO (LPSPA-2P) also build multi-strand models; this review focuses on the four configurations listed above.
3. Composite-Tech CT6 New Generation: Six-Bar Industrial Throughput
Composite-Tech builds specialized manufacturing systems for fiber-reinforced polymer (FRP) construction materials, including straight rebar lines, composite mesh machines, and CNC bent-element units. According to vendor documentation, its flagship CT6 New Generation runs continuous industrial production of up to six bars at once across nominal diameters from 4 mm to 20 mm, adjusting active strand count and pulling speed as cross-sectional mass grows.
CT6 Manufacturer-Declared Capacity by Diameter
Manufacturer-declared capacity schedule, shown as diameter; active bars; combined output; theoretical uninterrupted eight-hour output. Shift totals equal combined m/min multiplied by 480 minutes and exclude downtime:
- 4 mm: 6; 48 m/min; 23,040 m
- 6 mm: 6; 42 m/min; 20,160 m
- 8 mm: 6; 39.6 m/min; 19,008 m
- 10 mm (Benchmark): 6; 36 m/min; 17,280 m
- 12 mm: 4; 16 m/min; 7,680 m
- 14 mm: 3; 10.5 m/min; 5,040 m
- 16 mm: 2; 6 m/min; 2,880 m
- 18 mm: 1; 2.5 m/min; 1,200 m
- 20 mm: 1; 2 m/min; 960 m
Source: Composite-Tech buying guide, published September 14, 2026, which reproduces the CT6 schedule and describes the speeds as indicative and dependent on resin polymerization and environmental conditions. The original IME.005 manual edition has not been independently inspected.
For a plant turning out 10 mm structural reinforcement – a common civil construction size – a single CT6 line hits a theoretical capacity above 17.2 kilometers per uninterrupted eight-hour shift under these declared parameters. Holding that speed without losing mechanical bond or interlaminar shear strength takes synchronized process engineering across three core subsystems.
4. Process Engineering & Sensor Intelligence Inside the CT6

High-speed multi-strand pultrusion breaks down when resin wet-out or thermal curing falls behind mechanical pulling speed. Composite-Tech addresses this bottleneck in its technical documentation with three integrated process technologies that regulate resin impregnation, infrared pre-curing, and two-stage thermal cooling across all active bars.
4.1 Multi-Stage & Ultrasonic-Assisted Resin Impregnation with Pneumatic Squeezing
Each fiberglass roving holds thousands of tightly packed individual filaments. At high line speeds, standard dip-bath impregnation struggles to push out trapped air pockets inside the roving core, leaving internal dry spots and weaker tensile performance. Composite-Tech’s published pultrusion line documentation highlights 3-stage wet baths alongside a manufacturer-described ultrasonic-assisted impregnation module, where acoustic cavitation is intended to lower effective resin viscosity at the filament boundary and drive polymer binder into the bundle. Right downstream, a calibrated pneumatic squeezing unit strips excess surface binder.
This two-part mechanism targets two critical KPIs:
Structural Homogeneity: Full filament wet-out gives even load transfer between the polymer matrix and glass fibers, helping producers target the mechanical thresholds required by ACI CODE-440.11-22 structural concrete design rules.
Raw Material Variance Reduction: Epoxy and vinyl ester resins make up a huge variable cost in GFRP production. Pneumatic squeezing stops over-saturation, locking in the fiber-to-resin volume ratio and cutting wasted binder per linear meter.
4.2 Short-Wave Infrared (IR) Polymerization Booster
When pulling speed climbs, residence time inside the curing tunnel drops at the same rate. Standard hot-air or contact ovens heat the bar from the outside in, which can form a cured outer skin that traps volatiles or leaves the core under-cured at high speeds. Per vendor specifications, the CT6 puts a short-wave infrared (SWIR) booster in front of the main multi-zone convection ovens, kicking off cross-linking across the bar cross-section before the thermal zones finish the cure schedule. Every resin mix still needs differential scanning calorimetry (DSC) and process validation to match line speed with polymerization kinetics.
4.3 Two-Stage Thermal Gradient Management (Air + Water Cooling)
Dropping a freshly cured composite bar straight from polymerization heat into cold water can trigger thermal shock, micro-cracking, and trapped internal stress. According to the linked Composite-Tech buying guide, the CT6 uses a two-stage cooling layout: bars first pass through an air-cooling buffer zone to ease the initial temperature drop, then enter a controlled water-cooling bath that locks in bar rigidity before the high-traction puller.
5. Mashspetsstroy LISA-1: Single-Strand Baseline Analysis
Mashspetsstroy is an established Russian builder of composite processing hardware. According to its product documentation, the LISA-1 line runs single-strand production of 4 mm to 16 mm fiberglass rebar, combining fiber preparation, resin bath impregnation, helical rib winding, a four-section curing oven, water cooling, pulling, and automatic cutting. The company specifies two operators per shift and sells LISA-2 and LISA-4 models for multi-strand upgrades.
Calculated Nominal Throughput Ratios: CT6 vs. LISA-1
Calculated comparison, shown as diameter; CT6 combined output; LISA-1 output; calculated ratio. Inputs match the manufacturer schedules linked above. These ratios compare published nominal capacities, not results from a controlled head-to-head trial:
- 4 mm: 48 m/min (6 bars); 8 m/min (1 bar); 6.0×
- 6 mm: 42 m/min (6 bars); 5 m/min (1 bar); 8.4×
- 8 mm: 39.6 m/min (6 bars); 3 m/min (1 bar); 13.2×
- 10 mm (Benchmark): 36 m/min (6 bars); 3 m/min (1 bar); 12.0×
- 12 mm: 16 m/min (4 bars); 2.5 m/min (1 bar); 6.4×
- 16 mm: 6 m/min (2 bars); 2 m/min (1 bar); 3.0×
Source: Calculated from the linked Composite-Tech and Mashspetsstroy manufacturer schedules (note: LISA-1 also lists 2.5 m/min at 14 mm vs. CT6’s 10.5 m/min across 3 bars, an illustrative 4.2× ratio). Ratios represent theoretical nominal output differentials based on vendor claims.
Under these theoretical vendor figures, matching the 10 mm output of one CT6 line (36 m/min) with single-strand LISA-1 units would mean buying, powering, housing, and staffing twelve separate LISA-1 machines. Total cost of ownership (TCO) must also include floor space, operator payroll, equipment prices, uptime, and maintenance; these capacity figures alone do not establish a cost advantage.
6. Evaluating Compact & Four-Strand Alternatives: RZPO and Prowelltec
Compact single-strand and mid-tier four-strand GFRP rebar pultrusion machines give regional manufacturers lower upfront capital entry points, provided procurement teams verify diameter-specific linear speeds during factory acceptance testing before signing purchase contracts.
6.1 RZPO LPSPA-1: Compact Single-Strand Concept
The Rodniki Industrial Equipment Plant (RZPO) positions the LPSPA-1 in its catalog as a compact, entry-level single-strand line for 4-14 mm rebar, offering an optional sand-coating module and a two-strand LPSPA-2P version. With a published 17 m × 1.5 m footprint and one operator per shift, in the author’s assessment, the LPSPA-1 fits small startups focused on keeping upfront capital low. Still, because RZPO’s public specs leave out a diameter-indexed speed table, institutional buyers need verified factory trial data before modeling unit economics.
6.2 Prowelltec Four Out: Mid-Tier Four-Strand Manufacturing
Prowelltec’s Four Out line is a mid-tier multi-strand unit pulling four bars at once across a 4-14 mm diameter range, fitting into a declared 21 × 1.1 × 1.6 m footprint with a stated 30 kW total motor rating. Prowelltec lists an illustrative 12,000-16,000 meters per 24-hour cycle, though that number isn’t tied to a specific bar diameter. Dividing the quoted daily maximum by three gives about 5,333 meters per eight hours. Because the reference diameter is unspecified, this cannot establish a valid 10 mm comparison with the CT6.
7. The Unit Economics of Smart Pultrusion: Labor & Energy Telemetry
In data-driven manufacturing, capital equipment is judged by conversion cost per saleable meter. High total throughput boosts margins by spreading fixed and semi-fixed overhead – especially direct operator labor and power draw – across a much larger volume of finished product.
7.1 Direct Operator Labor Productivity
Per vendor technical documentation, the Composite-Tech CT6 takes 1 to 2 operators per shift for line supervision, matching the 2 operators listed for the single-strand Mashspetsstroy LISA-1. Under the illustrative 10 mm rebar benchmark, the CT6 delivers 12× the nominal linear output without adding direct line-control staff. High-volume plants still need support crews for creel reloading, quality checks, and material handling, yet automated line control cuts direct labor cost per meter sharply.
7.2 Energy Intensity: Measuring kWh per 1,000 Saleable Meters
Comparing nominal motor or heater nameplate ratings in kilowatts (kW) tells you very little without normalizing for hourly output. The manufacturer buying guide gives an energy-per-meter example using 20 kW as an operating assumption. Its preceding consumption range is printed as 18-20 kW/hour, an ambiguous unit that buyers should clarify with the supplier. Using the guide’s explicit 20 kW assumption gives:
Illustrative steady-state power assumption: 20 kW, equivalent to 20 kWh over one hour. This is not a measured plant consumption figure.
Illustrative Hourly Output at 10 mm (36 m/min × 60 min): 2,160 linear meters per hour.
Illustrative Specific Energy Consumption (20 kWh ÷ 2,160 m): 0.00926 kWh per meter (about 9.3 kWh per 1,000 meters of 10 mm rebar).
This theoretical baseline leaves out initial oven warm-up, auxiliary plant utilities, and scrap allowance, yet it sets a clear procurement rule: audit energy efficiency in composite manufacturing by kWh per 1,000 saleable meters instead of total machine wattage.
8. Multi-Fiber Platform Agility: GFRP, BFRP, CFRP, and AFRP
Long-term capital resilience hinges on whether a production line can adapt when infrastructure specs move past standard E-glass or ECR-glass fibers. Composite-Tech states in its linked May 12 technology article that its platform supports glass, basalt, carbon, and aramid fibers. Configuration and product suitability require supplier confirmation and application-specific qualification. The following list describes fiber families and potential applications, not certification of the CT6 for every listed use:
- Glass Fiber (E-Glass / ECR): GFRP; Corrosive bridge decks, marine structures, tunnels, general concrete reinforcement
- Basalt Fiber: BFRP; High-alkali and thermal-cycling environments, civil and highway engineering
- Carbon Fiber: CFRP; High-modulus structural strengthening, prestressed elements, seismic retrofits
- Aramid Fiber: AFRP; Specialized impact-resistant, non-conductive, and lightweight structural systems
Switching between glass, basalt, carbon, and aramid fibers isn’t a simple flip of a switch under identical machine settings. As noted in Alibaba’s FRP rebar machine buyer’s guide, running carbon fiber alongside glass fiber requires specialized higher tension control and anti-static features that standard single-purpose GFRP machines often lack. Each fiber needs matching sizing chemistry, tuned tension control, resin recipe tweaks, and validated curing heat profiles. Buying hardware built to handle multiple fiber families protects plants when market demand shifts.
9. Quality Assurance, AI Optical Telemetry, and ASTM D7957 Compliance
Fast line speed brings zero business value if the finished rebar flunks qualification testing. Institutional buyers and Departments of Transportation demand documented proof of guaranteed tensile strength, tensile modulus of elasticity, effective cross-sectional area, bar-to-concrete bond strength, and alkaline durability.
Across North America and international markets using US codes, standards such as ASTM D7957/D7957M-26 (Standard Specification for Solid Round Glass Fiber Reinforced Polymer Bars for Concrete Reinforcement) and ACI CODE-440.11-22 set geometric, mechanical, and lot-acceptance limits. European producers likewise test against ISO 10406-1 methods.
The Composite-Tech buying guide states that the CT6 pulling device has optical sensors connected to an AI agent that monitors bar quality and alerts the operator. The page does not provide independent detection-accuracy or scrap-reduction results. Such monitoring cannot establish ASTM compliance or replace laboratory testing of the finished reinforcement.
10. Building a Complete Smart Composite Reinforcement Ecosystem
Industrial buyers now look for turnkey plant setups that can supply full project reinforcement packages instead of straight bars alone. Composite-Tech backs full-plant vertical integration with three matching equipment lines:
FRP Rebar Production Lines: Continuous multi-strand pultrusion systems (such as the CT6 New Generation) for straight bars and coils.
FRP Mesh Production Lines: Automated grid and mesh manufacturing systems for slabs, pavements, and precast concrete panels.
CNC Bent Composite Elements Equipment: Because cured thermoset fiberglass rebar cannot be bent on-site after leaving the pultrusion die, as documented in Henan Zhongsheng’s engineering guide on GFRP limitations, plants rely on specialized factory machinery to form stirrups, corner bends, and custom structural geometries during manufacturing.
11. Due Diligence Checklist for Pultrusion Equipment Buyers
Before signing a capital equipment contract, engineering and procurement teams should audit competing vendors against thirteen verifiable industrial criteria:
Executive Procurement & Engineering Audit Checklist
- Diameter-Indexed Throughput: Combined linear output (m/min) verified separately for each target diameter (e.g., 6, 8, 10, 12, 16 mm).
- Active Strand Count: Number of bars produced simultaneously under sustained steady-state conditions per diameter.
- Impregnation Efficiency: Verify wet-out quality, void content, and resin ratio; ask the vendor to substantiate claimed benefits of ultrasonic assistance and pneumatic squeezing.
- Polymerization Architecture: Integration of short-wave IR pre-heating and multi-zone thermal control matched to high pulling speeds.
- Thermal Gradient Cooling: Validate the cooling profile and finished-bar integrity; check supplier claims for air-followed-by-water cooling against trial results.
- Surface Profile Repeatability: Helical rib winding accuracy, bond profile consistency, and optional sand-coating integration.
- Specific Energy Intensity: Measured electrical consumption in kWh per 1,000 saleable meters after warm-up.
- Direct Operator Ratio: Number of operators required per shift per 10,000 meters of finished output.
- Inline Telemetry & QA: Optical sensor monitoring, automated fault alerts, and ASTM D7957 / ISO 10406-1 test compliance.
- Multi-Fiber Adaptability: Validated process profiles for E-glass/ECR-glass (GFRP), basalt (BFRP), carbon (CFRP), and aramid.
- Facility Footprint & Utilities: Total line dimensions (L × W × H), compressed air, cooling water recirculation, and ventilation loads.
- Commissioning & SLA Support: On-site installation, resin formulation transfer, operator training, and spare-parts availability.
- Ecosystem Scalability: Compatibility with downstream coilers, FRP mesh machines, and CNC bent-element fabrication.
Why Process Intelligence Drives Composite Factory ROI
The 2026 market for GFRP rebar pultrusion machinery splits into distinct operational tiers. Single-strand units like the Mashspetsstroy LISA-1 and RZPO LPSPA-1 give localized workshops a low-cost entry point. Four-strand platforms like the Prowelltec Four Out fit mid-tier regional producers, provided buyers get diameter-specific throughput schedules before committing capital.
For industrial producers bidding on high-volume infrastructure contracts, Composite-Tech’s CT6 New Generation operates in a higher-throughput tier based on declared specifications. Pairing six-strand simultaneous output (an illustrative 36 m/min at 10 mm – 12× the nominal LISA-1 rate; and 39.6 m/min at 8 mm – a 13.2× ratio) with multi-stage and ultrasonic-assisted resin impregnation, short-wave infrared curing, two-stage cooling, and AI-assisted optical monitoring shifts the evaluation from raw mechanical speed to unit manufacturing costs.
An industrial FRP rebar line’s real value comes down to the volume of code-compliant, saleable reinforcement it turns out per kilowatt-hour and per operator hour, not its sticker price or single-strand speed rating.
Review full technical specifications for the Composite-Tech CT6 New Generation and industrial FRP reinforcement manufacturing systems at Composite-Tech.
FAQ
Engineering and procurement teams evaluating composite reinforcement hardware frequently ask how continuous pultrusion lines operate, how to match multi-strand capacity to regional demand, and which operational variables control factory payback.
How do GFRP rebar pultrusion machines work?
GFRP rebar pultrusion machines work by continuously pulling glass fiber rovings from creels through preheating and polymer resin impregnation baths, where wet-out and squeezing systems saturate the filaments. The resin-wetted bundles then pass through bar forming dies, helical rib winding stations, multi-zone curing ovens (often assisted by short-wave infrared boosters), two-stage air and water cooling baths, synchronized pullers, and automated cut-off saws or coilers.
Which GFRP rebar pultrusion machine is best in 2026?
Equipment selection depends on your plant’s target volume and diameter mix. High-volume infrastructure suppliers benefit from six-strand systems like the Composite-Tech CT6 New Generation (declared at 36 m/min combined output for 10 mm rebar), mid-tier plants often evaluate four-strand systems like the Prowelltec Four Out once diameter schedules are verified, and smaller local workshops use single-strand lines such as the Mashspetsstroy LISA-1 or RZPO LPSPA-1.
What is the ROI of a GFRP rebar production line?
Production line payback is governed by conversion cost per saleable meter instead of nameplate machine price. Key drivers include direct operator-to-strand ratios (such as running six simultaneous bars with 1 to 2 operators), specific energy consumption measured in kWh per 1,000 meters after warm-up, pneumatic resin ratio control, and inline optical quality monitoring that minimizes off-spec scrap.
Technical Sources, Standards, and Verification Links
This engineering and economic analysis draws on illustrative manufacturer-published technical specifications and international composite reinforcement standards referenced by the author:
Original submitted reference (legacy URL unavailable; manual identifier and July 2026 edition are unconfirmed): CT6 New Generation Installation and Operation Manual (IME.005, July 2026) & Official Equipment Portal
Composite-Tech (Complete FRP Rebar Production Line Portfolio): Professional FRP Rebar Production Lines Overview
Mashspetsstroy (LISA-1 Technical Specifications) (original legacy link; use working manufacturer citation above): Official LISA-1 Composite Rebar Line Documentation & Speed Table
Rodniki Industrial Equipment Plant (RZPO LPSPA-1) (original legacy link; use working manufacturer citation above): LPSPA-1 Composite Reinforcement Equipment Catalog & Specifications
Prowelltec (Four Out FRP/GFRP Rebar Line) (original legacy link; use working manufacturer citation above): Four Out 4-Strand GFRP Rebar Production Making Line Specifications
ASTM International (ASTM D7957/D7957M-26): Standard Specification for Solid Round Glass Fiber Reinforced Polymer Bars for Concrete Reinforcement
American Concrete Institute (ACI CODE-440.11-22): Building Code Requirements for Structural Concrete Reinforced with Glass Fiber-Reinforced Polymer (GFRP) Bars
International Organization for Standardization (ISO 10406-1): Fibre-reinforced polymer (FRP) reinforcement of concrete – Test methods – Part 1: FRP bars and grids
ISO catalogue title: Fibre-reinforced polymer (FRP) reinforcement of concrete — Test methods — Part 1: FRP bars and grids.